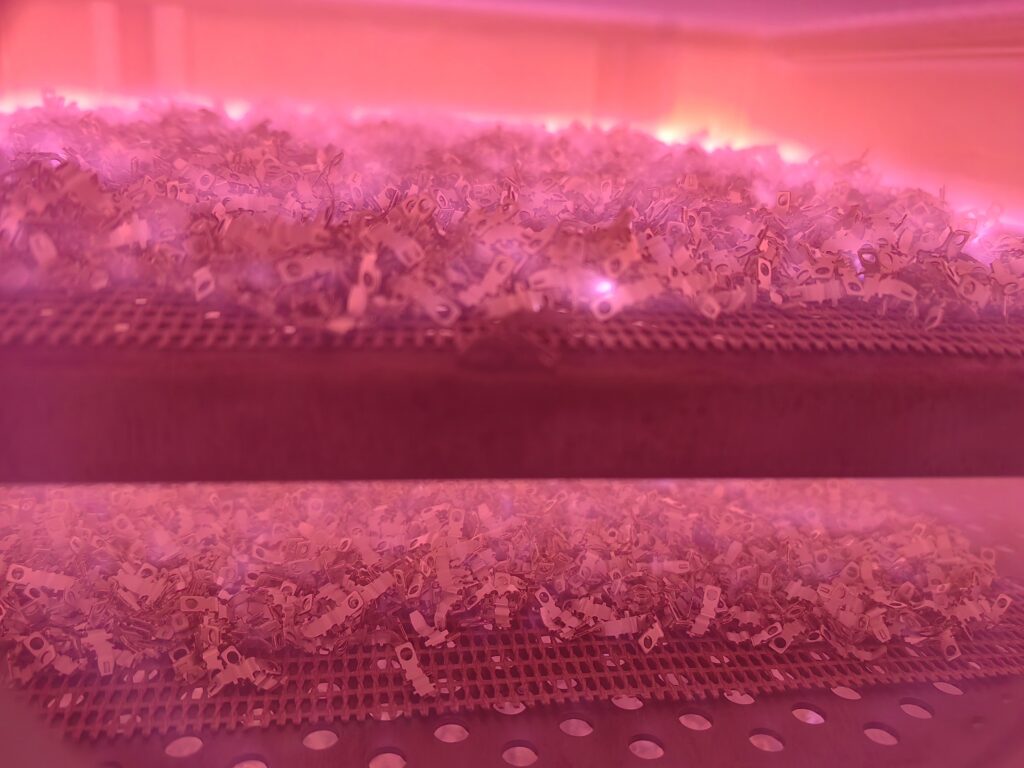
Plasma cleaning for aluminum parts is a dry option for removing trace oils and preparing selected aluminum surfaces before bonding, coating, printing or other assembly steps. It is especially valuable when solvent wiping removes visible oil but leaves variable wetting, when water cleaning adds a drying burden, or when a precision part cannot tolerate aggressive abrasion.
Aluminum naturally develops an oxide film in air. The engineering question is not whether every oxide atom can be removed, but whether the process can remove the weakly bound contamination and condition the interface consistently for the next operation. Recipe development must distinguish organic cleaning, oxide modification and surface activation.
Machining oil, cutting fluid, forming lubricant, release agent and fingerprints can collect in pores, parting lines and small recesses. Solvent cleaning may remove free oil while leaving a chemically different surface and a recontamination risk during drying. Mechanical cleaning can change roughness or create particles. Water-based cleaning requires rinsing, drying and wastewater controls.
For a broader explanation of interface failures, see why adhesive bonds fail at the surface. Plasma is most effective when the defect analysis shows that contamination or wetting is limiting the downstream process.
Reactive plasma species interact with the outer surface. A validated process may:
The effect depends on gas chemistry, power, pressure, time and part temperature. Our guide to cleaning, activation and etching helps separate these mechanisms. Over-treatment can increase roughness, alter appearance or change a surface that was intentionally protected.
Plasma can be placed before structural adhesive, sealant, gasket bonding or thermal-interface attachment. Confirm lap shear, peel, cohesive failure, environmental aging and the maximum delay before dispensing.
Activation may improve wetting of a compatible primer or coating. It does not replace surface design, corrosion protection or cure control. Test gloss, color, adhesion and corrosion performance after the complete finish stack.
Vacuum plasma can provide more uniform exposure around complex geometries, while atmospheric nozzles are efficient for open surfaces and inline tracks. Deep blind holes and narrow grooves need a fixture or chamber study; a flat-panel result cannot be transferred automatically.
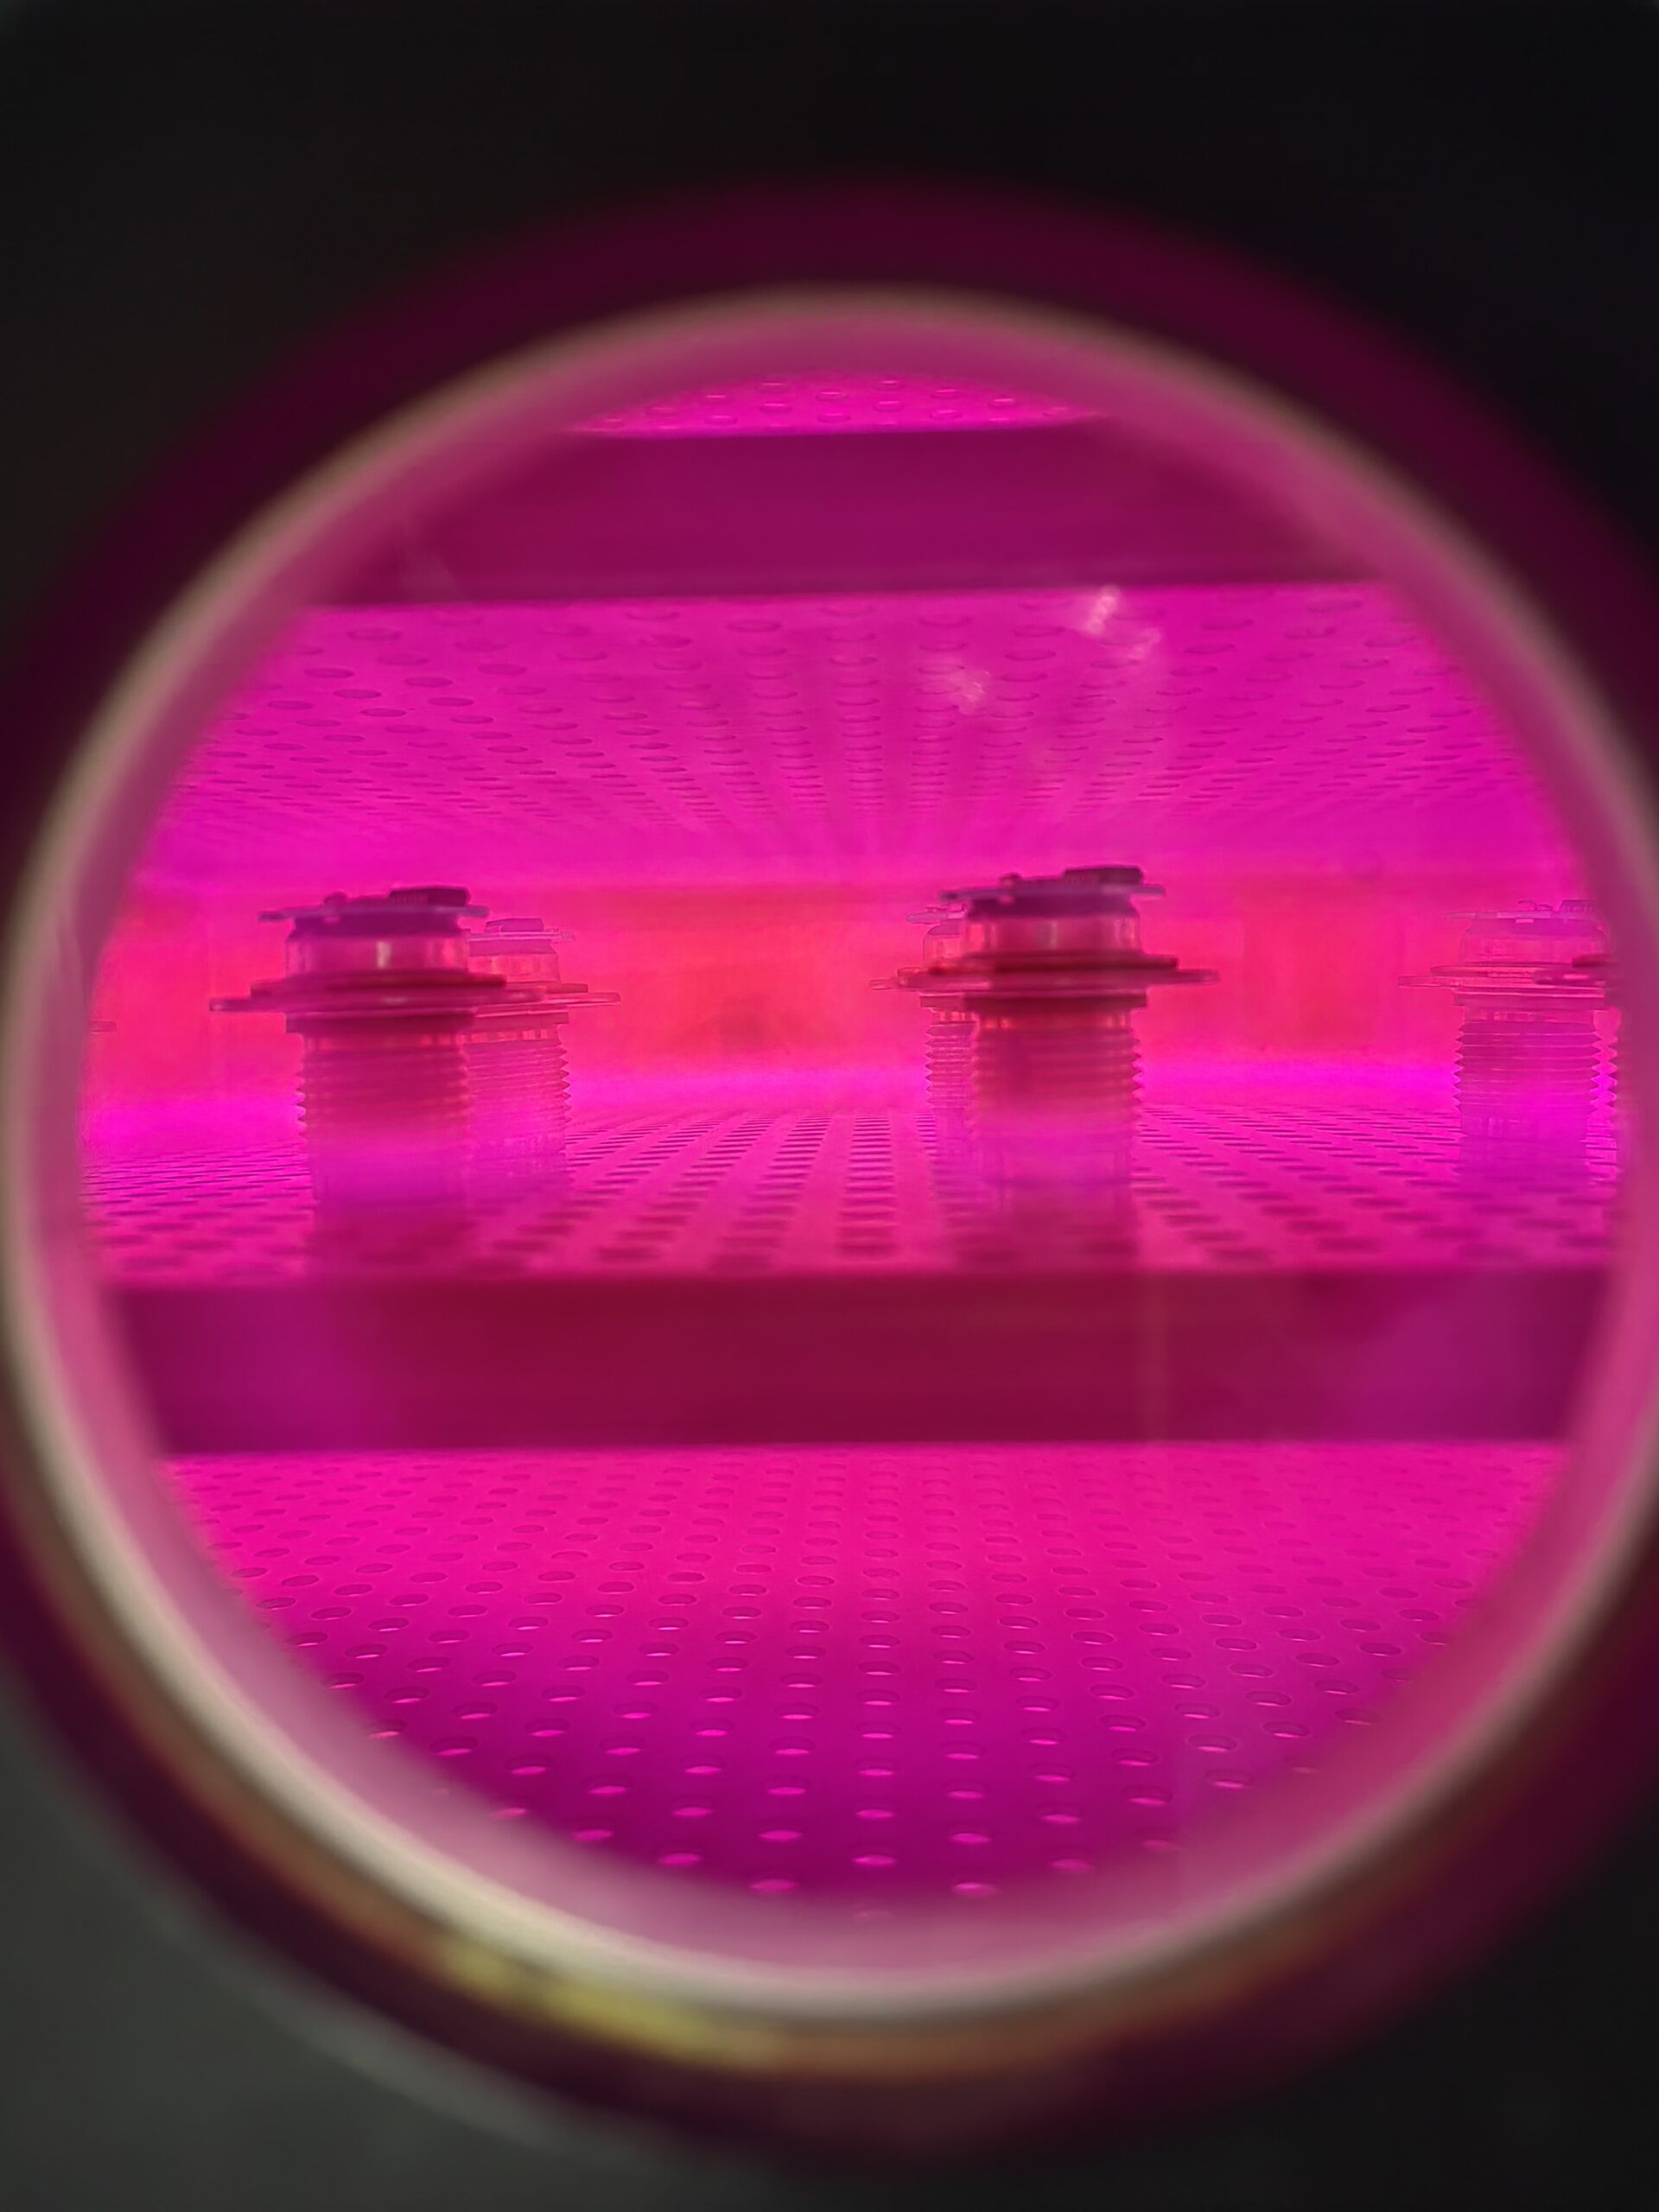
Use the gas-selection guide to compare air, oxygen, nitrogen and argon options, then select the chemistry that supports the downstream interface.
Measure the untreated baseline and test multiple treatment doses on representative alloys, finishes and contamination levels. Contact angle or dyne measurements are useful screens, but the acceptance test should be the actual bond, coating, weld or seal. Include part storage, handling, supplier lots and tool maintenance in the study.
Aluminum can re-form oxide after exposure to air, so the treatment-to-process delay is part of the recipe. Use defined packaging or proceed directly to the next operation. The limits of surface-energy measurement methods are important when interpreting a high reading that does not translate into bond strength.
Not necessarily, and that is rarely the right specification. The process can remove contamination and modify a thin surface layer, but oxide composition and thickness must be characterized for the actual alloy and downstream process.
Aluminum remains reactive in air. Re-oxidation and recontamination can occur, so bond, coat or seal within a qualified window and control handling.
Vacuum treatment is often easier to make uniform around recessed features. Atmospheric jets may have limited reach in deep blind holes; fixture design and verification are essential.
A controlled process is intended to have minimal bulk effect, but excessive dose can change roughness, gloss or color. Check dimensional accuracy, surface finish and temperature on production parts.
No. Plasma can replace or reduce a wet step when the trial proves equivalent or better performance and the facility validates safety, exhaust, cleanliness and quality requirements.
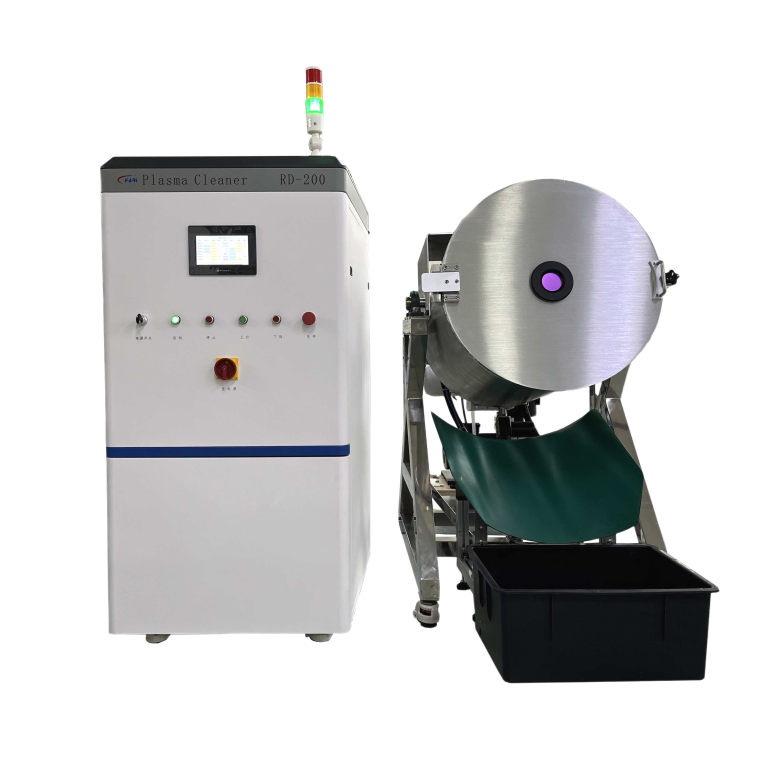
FARI Plasma can compare atmospheric and vacuum formats, map a treatment window and connect the process to an existing line. Review inline integration considerations, browse available systems or contact us with the alloy, contamination, geometry and downstream test.
English
Spanish
Rogatus ad ultimum admissusque in consistorium ambage nulla praegressa inconsiderate