A Tier-1 supplier moved to inline plasma treatment for automotive bumper bonding, replacing chemical primer on a polypropylene line. The switch cut per-part surface-prep cost by more than 30% and took VOC emissions out of that process step entirely.
The bumper line ran a standard sequence: spray a solvent-based primer onto the bond flange, flash it off in a forced-air oven for 45–90 seconds, then send the part to adhesive dispensing. Every step added time, labor, and a chemical liability the plant had to manage — mixing stations, booth ventilation, hazardous-waste pickup, and a pot-life window that could turn a stopped line into scrapped parts. Tightening VOC limits also turned primer into a standing compliance risk rather than a one-time fix.
Removing that primer step cut per-part surface-prep cost by more than 30%, with the full comparison — primer material, labor, and disposal against the plasma line's power and gas draw — worked out in chemical primer vs. plasma treatment costs.
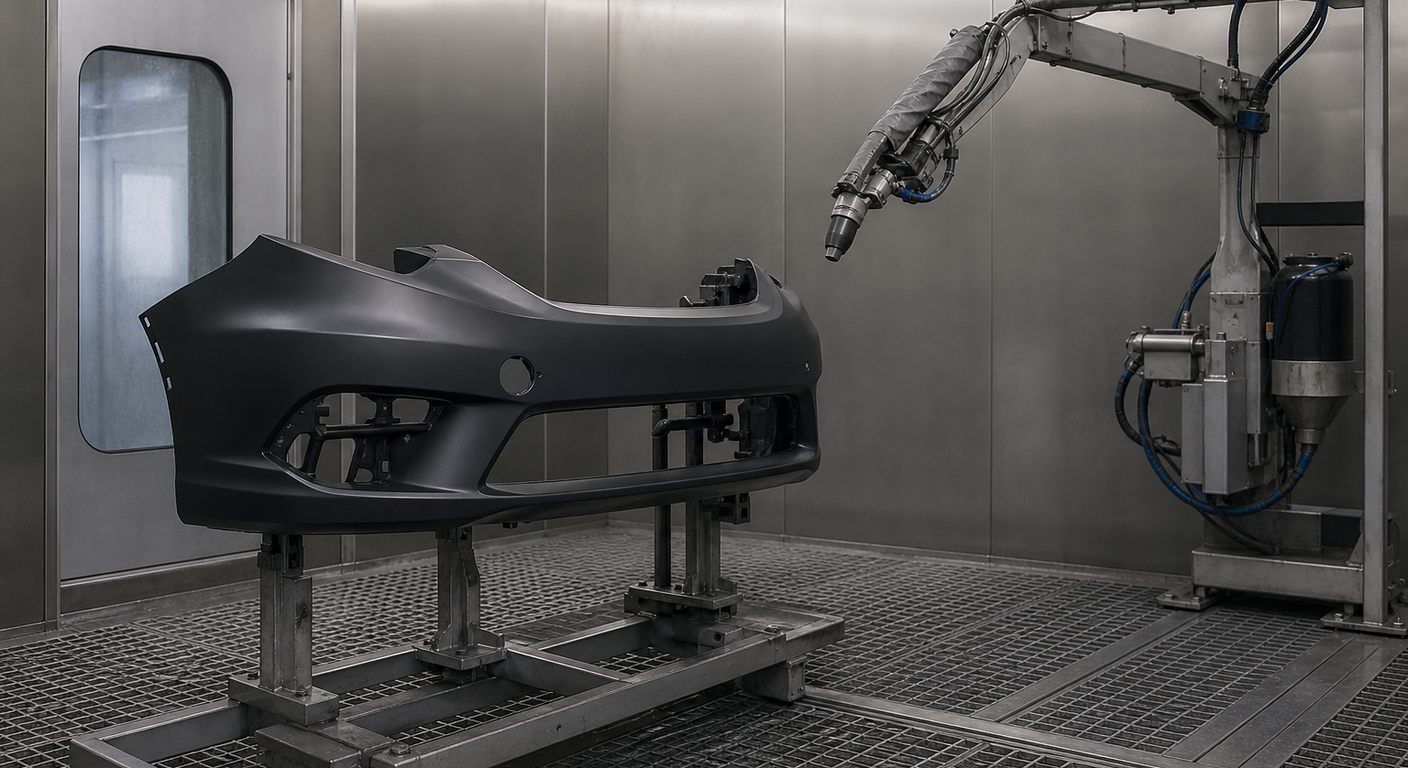
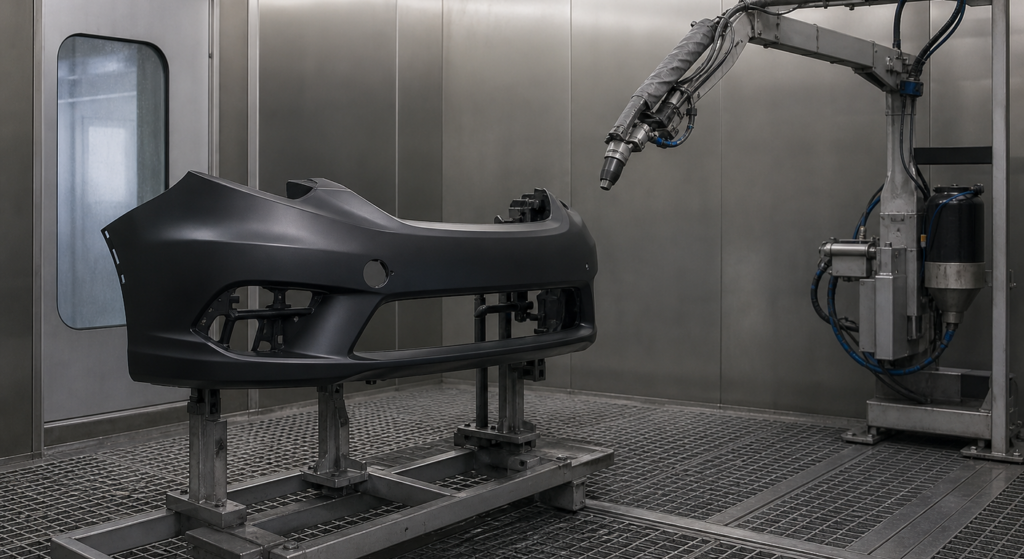
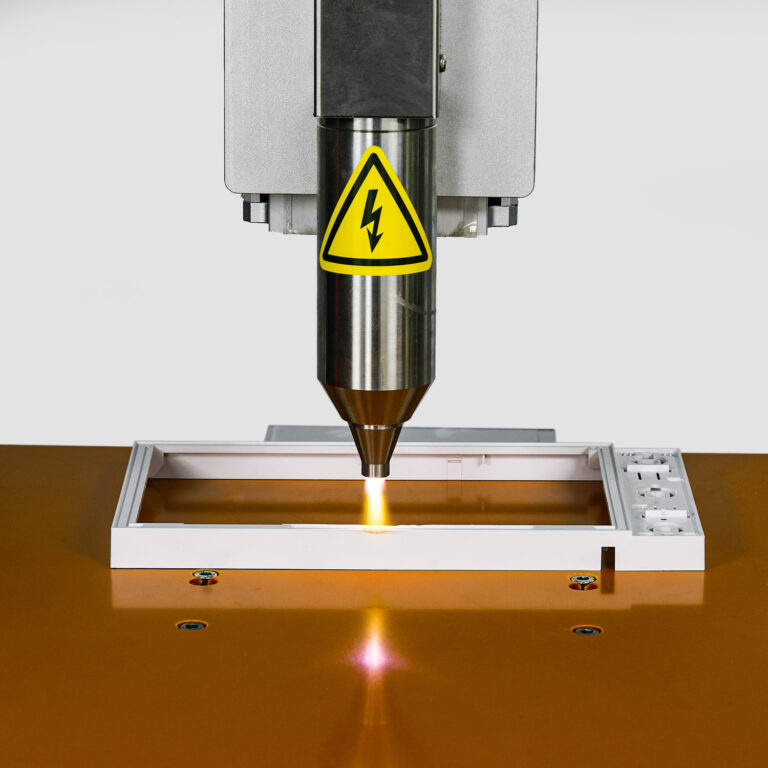
The line needed to treat a bond flange inside a fixed takt window, with the robot arm already dedicated to loading and adhesive dispensing. A vacuum plasma chamber would have meant pumping down and venting for every part — dead time this line didn't have. Atmospheric plasma runs at ambient pressure, so a plasma head mounted directly on the robot arm activates the flange between stations with no chamber cycle at all.
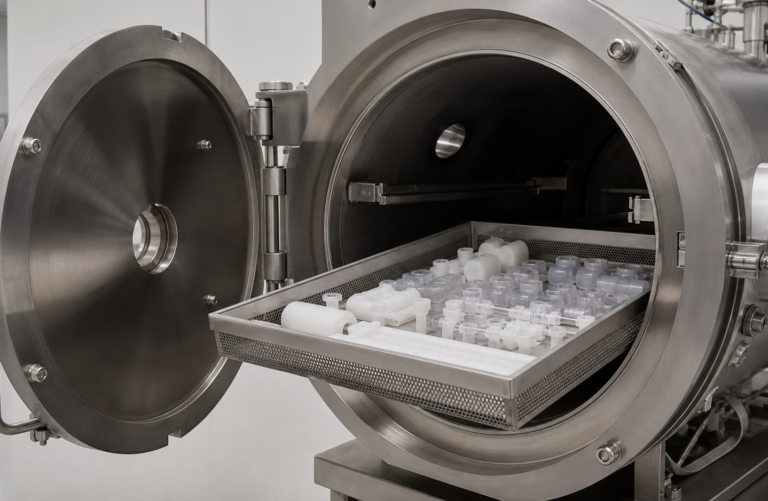
That trade-off reverses for small, complex-geometry parts that fit inside a chamber, where an inline automatic vacuum plasma cleaner treats every surface of a part at once instead of tracing a nozzle path across it — a better fit for discrete batch components than for a continuous bond flange.
Corona treatment was also evaluated and dropped: it handles flat film well but loses uniformity on the 3D bond flanges and deep-drawn contours this bumper needed, a gap covered in why plasma treatment options outperform corona in this case. The same integration logic carries across other vehicle assemblies, detailed in plasma treatment for automotive and aerospace applications.
The plasma head shares the robot arm that carries the adhesive dispensing valve, so the treatment path and the bond path run on one program instead of two separate stations. A four-nozzle atmospheric array, running in the 1–5 kW adjustable power range at 40 kHz and fed on compressed air rather than a specialty gas, traces the bond flange at 200–400 mm/s, holding a 5–15 mm standoff, and clears each flange in 8–12 seconds — inside the line's 42-second takt window. The robot moves directly from the treated flange to the two-component polyurethane structural adhesive valve, so there's no drying oven and no staging step where the surface has time to lose activation.
The compressed-air choice came out of a gas-selection trial: it produced enough surface-energy gain for the PP/EPDM blend without adding a cylinder-swap schedule to a line that already ran tight on floor space, a comparison laid out in how gas selection affected treatment results.
Three things moved once the plasma cell replaced the primer booth:
The plant confirmed the switch with lap shear peel testing against the production adhesive and a cataplasma aging test — cycling parts at elevated temperature and humidity — before releasing the process to full volume.
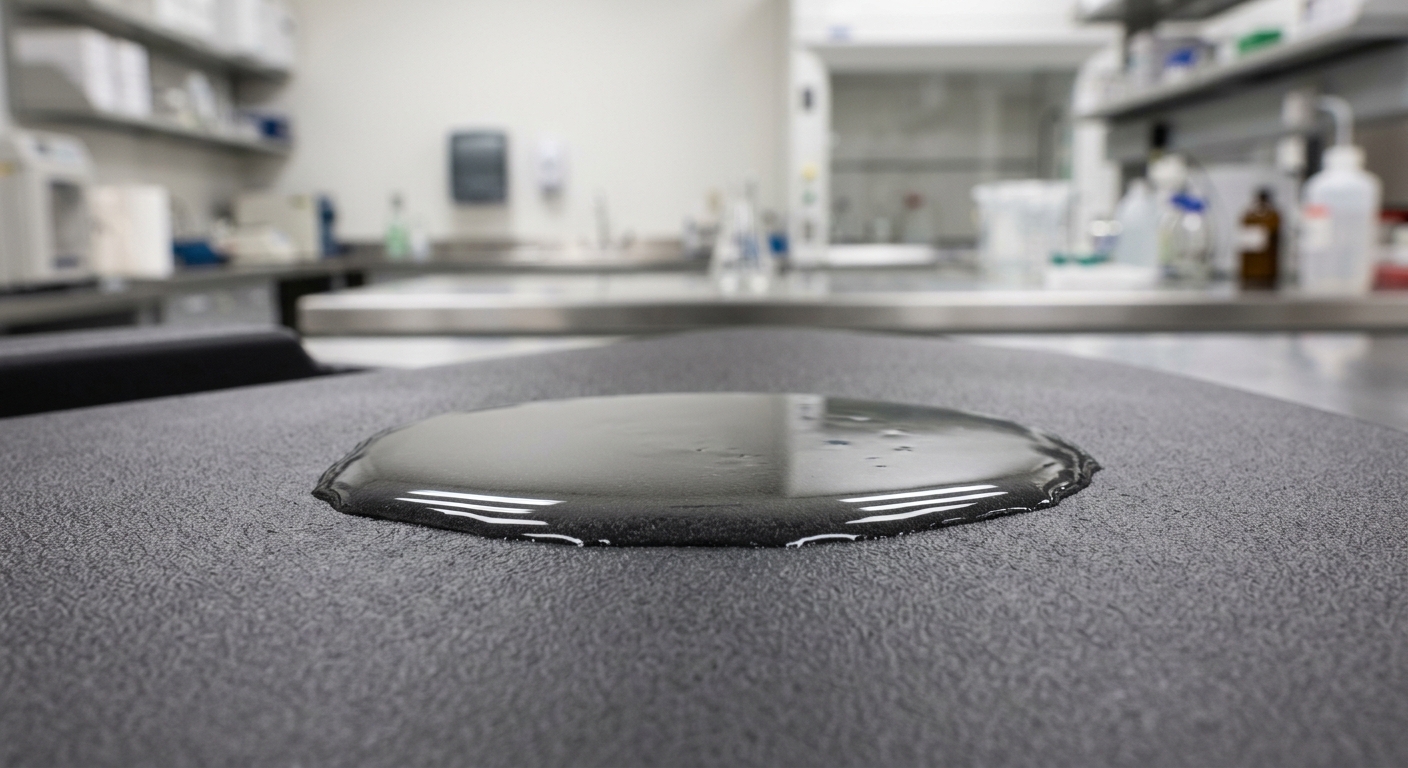
Every flange is checked with a contact angle reading before it reaches the adhesive station, not spot-checked on a sample basis. The process gate requires a reading below 30°; three consecutive readings above 35° flag the nozzle for cleaning or inspection before production continues. How surface quality was verified after treatment covers how that measurement is taken and read on the line.
Start by mapping three things against your own line: the substrate (polyolefins and most engineering plastics respond well; PTFE and silicones don't activate the same way), the step you're trying to replace (primer, flame treatment, or a manual wipe-down), and the takt time budget available for a treatment pass. If those line up, run the numbers with calculate your primer-to-plasma cost savings, then check equipment pricing on its own in Plasma Treatment System Cost 2026 before specifying hardware. For where else on the vehicle this fits — headlamp lenses, interior trim, gasket sealing surfaces — see full automotive plasma treatment applications.
The same before/after discipline shows up outside automotive. A consumer electronics line documented its cleaning switch in Plasma Cleaning Cuts Scrap 34%: Case Study, a medical device manufacturer tracked rejection-rate changes after switching prep steps in Plasma Cleaning Cut Medical Device Rejections 40%, and flexible packaging converters rely on the same activation mechanism to hold ink and coating adhesion, covered in Plasma Treatment for Flexible Packaging.
Contact our team to discuss a feasibility check for your bond, paint, or coating step.
What are the disadvantages of plasma treatment?
It adds a step to the line — a robot or fixed nozzle, a gas supply, and floor space for the head and controller. Every new material or part geometry needs its own process validation before production, and atmospheric systems still depend on stable gas logistics. It removes the primer's chemical handling burden, but it isn't a zero-cost drop-in.
How long does the plasma treatment last?
The activation effect fades over time through hydrophobic recovery — the surface's raised energy gradually drops back toward its original state if the part sits untouched. That's why this line treats and bonds within seconds of activation rather than staging treated parts for later use; inline integration removes the waiting period that would otherwise undo the effect.
How much does a plasma fusion treatment typically cost?
A single-nozzle atmospheric system with generator, gas supply, and mounting hardware typically runs in the tens of thousands of dollars; a multi-nozzle robotic array with process monitoring, like the four-nozzle setup described above, runs several times that once integration engineering is included. Plasma Treatment System Cost 2026 breaks the ranges down by configuration.
What does plasma treatment do?
It uses ionized gas to clean and activate a surface at the molecular level — removing contaminants and adding polar functional groups that raise surface energy so adhesives, paints, and coatings bond without a primer layer. The same core technology, run with a different gas and chamber setup, also performs plasma resist removal in electronics manufacturing.
If your line has a primer, flame-treatment, or manual wipe-down step that's adding cost or variability, contact fariplasmatech to walk through whether inline plasma fits your parts and your takt time.
English
Spanish
Rogatus ad ultimum admissusque in consistorium ambage nulla praegressa inconsiderate