An untreated BOPP, PE, or PET film surface is a non-polar hydrocarbon chain with no chemical site for an ink binder, adhesive, or coating resin to bond to. That fact explains most flexible-packaging adhesion complaints: ink beading, coating crawl, laminations that delaminate during pouch-filling. Plasma treatment for packaging films fixes it by chemically altering the surface before anything touches it. Below: how the treatment works film by film, and where it beats the corona treater most lines already have.
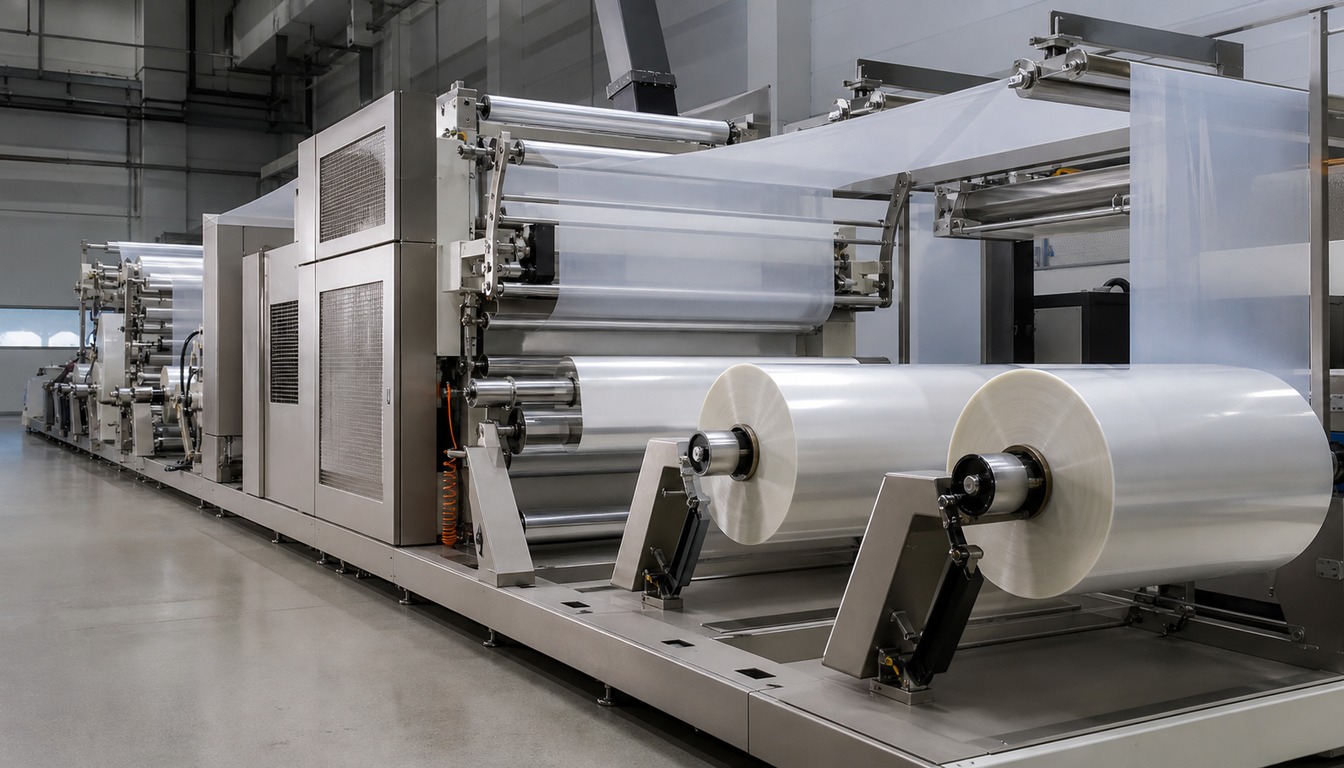
BOPP, PE, and PET run well at speed and deliver good barrier performance — that's why converters use them. Bonding easily isn't part of the deal. Their surfaces carry no polar functional groups, so ink binders, coating resins, and laminating adhesives have nothing to grip chemically. Roughening the surface doesn't help; the problem is missing chemistry, not missing texture.
The symptoms show up downstream: ink lifting on a tape-pull check, coatings crawling instead of laying flat, laminations failing under flex during filling, blocking where rolls stick together because slip agents migrated to the surface in storage.
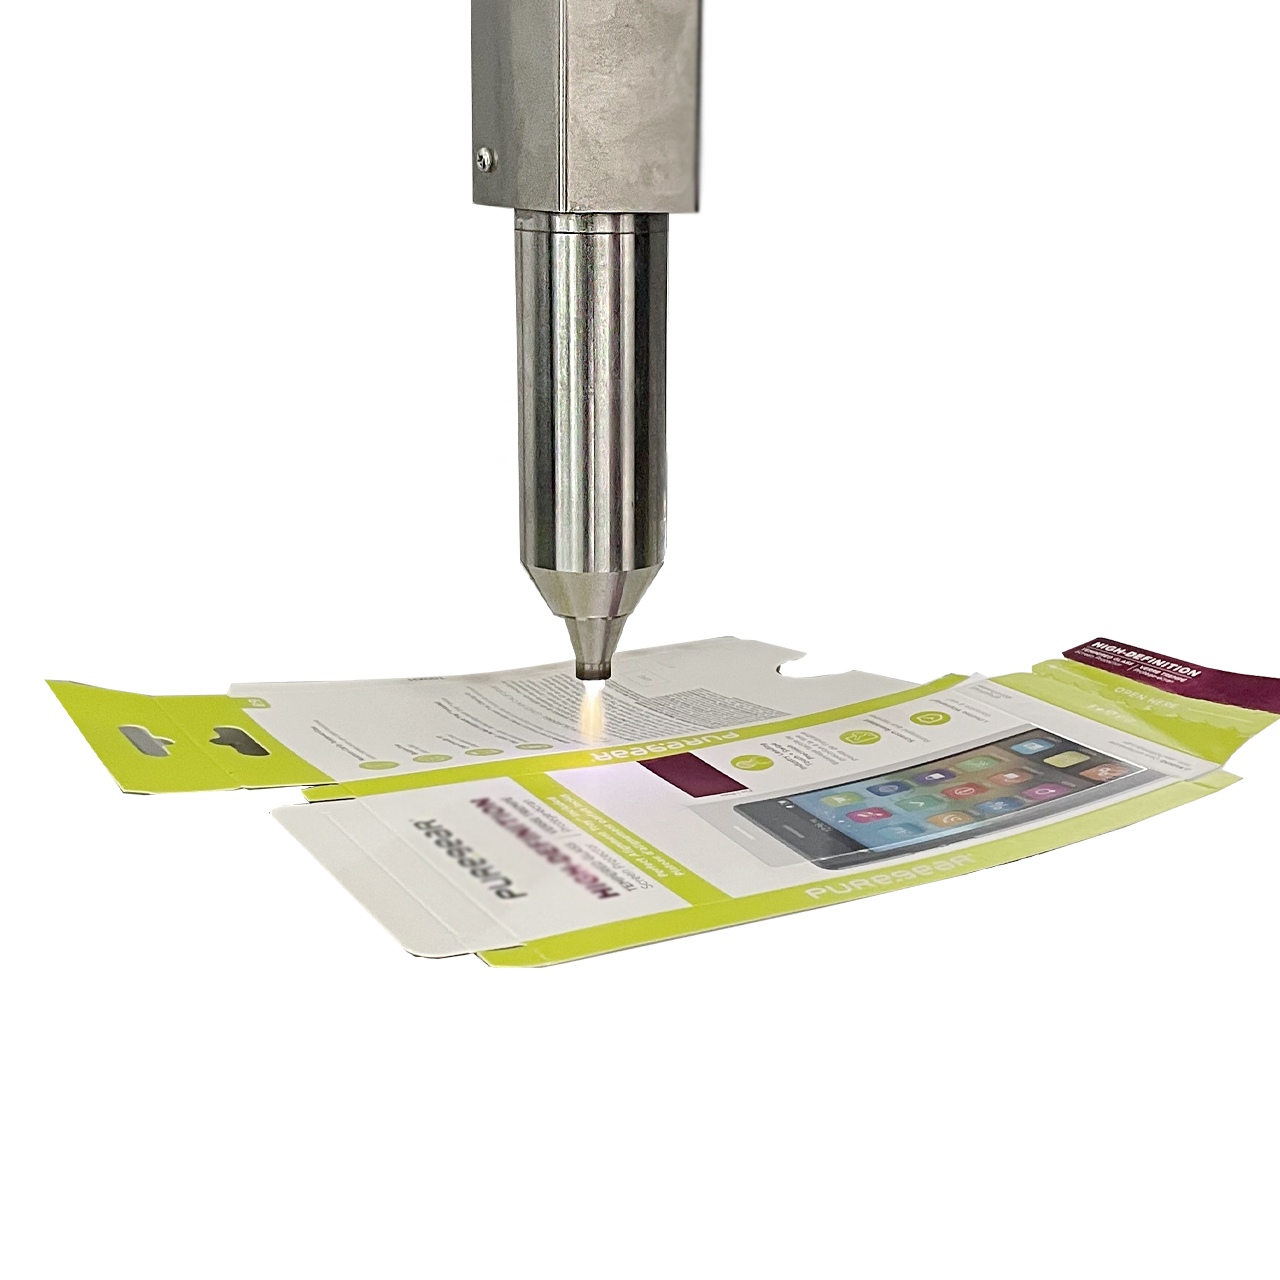
Plasma treatment exposes the film to an ionized gas of free radicals and reactive species. On contact, it strips contaminants and slip-agent bloom, then grafts polar functional groups onto the polymer backbone — raising surface energy so ink, coating, or adhesive wets out and bonds chemically instead of sitting on top.
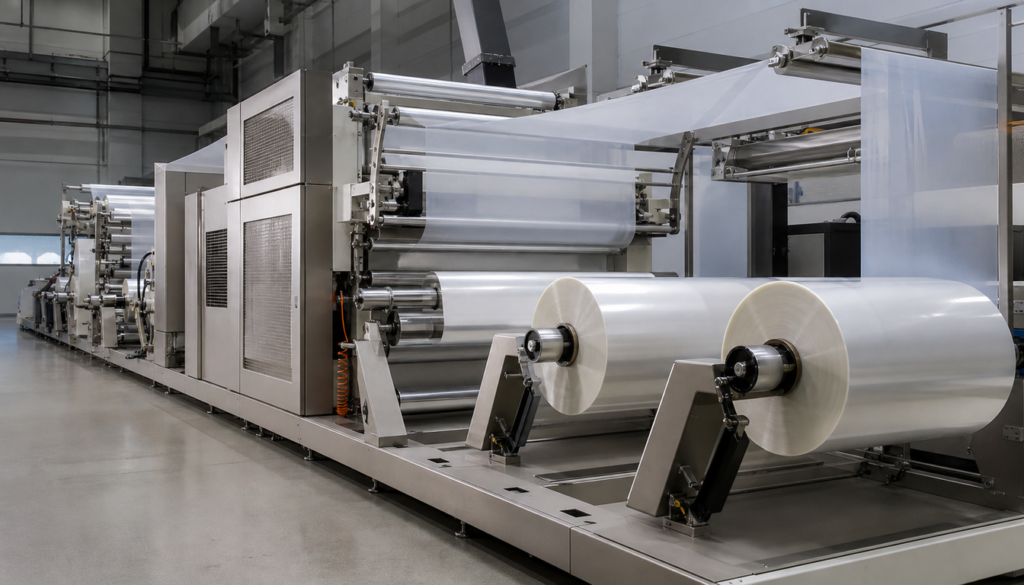
Atmospheric plasma is the format built for continuous web lines, since it runs inline at ambient pressure rather than in a sealed chamber. Process gas changes the chemistry grafted onto the surface — air, oxygen, and nitrogen chemistries each functionalize the surface differently, and matching gas to your ink or adhesive system matters more than most converters assume. The same plasma surface treatment mechanism — cleaning, then functionalization — behaves differently on each substrate, and activation, cleaning, and etching remain distinct processes with different jobs.
Corona handles a large share of flexible-packaging jobs adequately. It falls short in three situations: thin-gauge webs, where the discharge can penetrate through and damage backside heat-seal; delayed printing or lamination, where corona-treated surface energy decays as polymer chains rearrange and can drop below what an ink requires within a day or two of treatment; and metallized or complex laminates, where corona's discharge is harder to control uniformly across the web.
In these cases, plasma is the upgrade path — not a blanket replacement for corona on every line. Its confined discharge zone avoids backside treatment, and the functional groups it grafts hold longer before the next process step. The corona vs. plasma comparison shows when each treatment makes sense on a converting line.
BOPP is the most commonly plasma-treated packaging substrate, widely used for snack and confectionery wraps. Ink and coating suppliers commonly specify a surface-energy floor around 38–42 dyne/cm for reliable wet-out on BOPP — a widely cited industry benchmark, not a fixed rule for every ink formulation.
PET starts with higher inherent surface energy than BOPP or PE, but barrier coatings and metallization often demand more than the untreated film provides. Nitrogen-based chemistries tend to help specifically with these bonds.
PE (LDPE/LLDPE) is the hardest to functionalize because of its branched molecular structure. Treatment timing relative to storage matters as much as the treatment itself — PE loses surface energy through hydrophobic recovery faster than BOPP or PET.
Metallized and foil laminates benefit most when treatment happens immediately before adhesive lamination, since any gap between treatment and bonding works against you as activation fades.
A worked example: a BOPP web treated inline with air plasma, positioned directly ahead of a gravure print station, reaches surface energy above the 38–42 dyne/cm ink-wetting threshold and holds it because ink contact happens seconds later — not hours or days after treatment, which is when a primer step would otherwise be needed as insurance.
Plasma treatment belongs immediately before the step it protects — before print, before extrusion coating, before lamination. The closer it sits to that contact point, the less opportunity surface energy has to decay or contamination to redeposit.
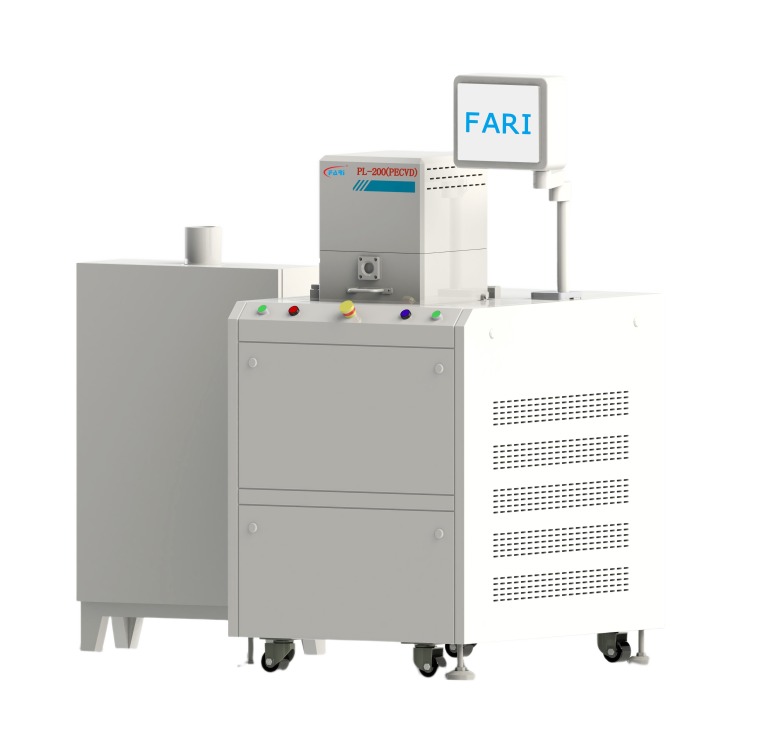
Atmospheric plasma suits continuous web processing; vacuum plasma is a batch process for parts or pre-formed trays loaded into a chamber, not a moving web. Vacuum plasma treatment applies instead of atmospheric when the product is a tray, container, or cut sheet rather than a web. Fari's packaging and printing plasma systems and atmospheric plasma treatment systems cover the inline web case.
Skipping verification is how under-treatment turns into a failed production run. Dyne ink testing, commonly run to ASTM D2578, is the quick shop-floor check: an ink of known surface tension is drawn across the film, and if it wets out and holds for a couple of seconds, the surface is above that rating. Contact angle measurement is more repeatable, reading how a water droplet sits on the surface rather than relying on operator judgment.
Contact angle measurement after plasma treatment is the fastest in-line check, and dyne ink, contact angle, and XPS are compared side by side — including lab-based XPS for cases where dyne or contact angle readings look fine but adhesion still fails.
Sizing a plasma system comes down to a short set of questions: which film types run through your line and in what mix, whether you're retrofitting alongside an existing corona treater or integrating fresh, and which process step is currently causing the adhesion problem. Those answers determine gas chemistry, line placement, and whether atmospheric or vacuum plasma fits. Send our team your film types and current adhesion issues, and we'll work out what a setup needs to look like for your line.
What is plasma treatment used for in flexible packaging?
It raises the surface energy of films like BOPP, PET, and PE so inks, coatings, and lamination adhesives wet out and bond instead of beading, crawling, or peeling off. Plasma grafts polar chemical groups onto an otherwise non-polar polymer surface to make that bond possible.
Does plasma treatment work on BOPP film?
Yes. BOPP is one of the most commonly plasma-treated flexible packaging films because its untreated surface energy sits well below what most inks and coatings require. Treatment is applied just before printing or laminating, where adhesion failures on BOPP most often surface.
How is plasma treatment different from corona treatment for packaging films?
Corona uses ambient-air discharge and works on most lines, but can treat through thin films and loses activation faster than plasma over hours to days. Plasma confines the discharge more precisely, avoids backside treatment, and holds its functionalization longer before the next process step.
Can plasma treatment replace primers on flexible packaging film?
In some cases, yes — plasma adds no additional layer or chemical coating, and can raise surface energy enough to eliminate a primer used purely as an adhesion safety net. Whether it fully replaces a primer depends on the specific film, ink, and adhesive system in use.
How long does plasma treatment’s effect on adhesion last before printing or laminating?
Treated surfaces lose activation gradually through hydrophobic recovery, as polymer chains rearrange and bury the grafted polar groups. That's why plasma treatment performs best placed immediately before the next process step, rather than treating rolls far in advance.
What causes ink or coating to peel off packaging film even after treatment?
Common causes include heavy surface contamination that overwhelmed the treatment, the wrong process gas chemistry for the specific ink or adhesive system, or storing treated film too long before use so activation decays before the next step.
How do you test whether plasma treatment worked on packaging film?
Dyne ink pens, run to a standard like ASTM D2578, give a quick shop-floor read on wettability; contact angle measurement is more consistent and operator-independent. For adhesion problems despite acceptable readings, lab-based surface chemistry analysis identifies whether the right functional groups are actually present.
Is plasma treatment safe for food-contact packaging film?
Plasma treatment modifies the existing polymer surface rather than depositing a new chemical layer, which is relevant for food-contact considerations. Regulatory compliance for any specific film, ink, and packaging structure still needs confirming for your product and jurisdiction.
Can plasma treatment be added inline on an existing printing or laminating line?
Atmospheric plasma systems are built for inline placement on continuous web lines, positioned just upstream of the print, coating, or lamination station. Integration specifics — placement, gas supply, control interfaces — depend on your existing line layout.
What packaging film types benefit most from plasma treatment (BOPP, PET, PE, foil)?
BOPP and PE benefit most because their untreated surface energy is lowest. PET benefits particularly where barrier coatings or metallization need stronger adhesion, and metallized or foil laminates benefit most when treatment happens right before adhesive lamination.


English
Spanish
Rogatus ad ultimum admissusque in consistorium ambage nulla praegressa inconsiderate